Dairy Bag-In-Box Packaging from Suzhou Jingle
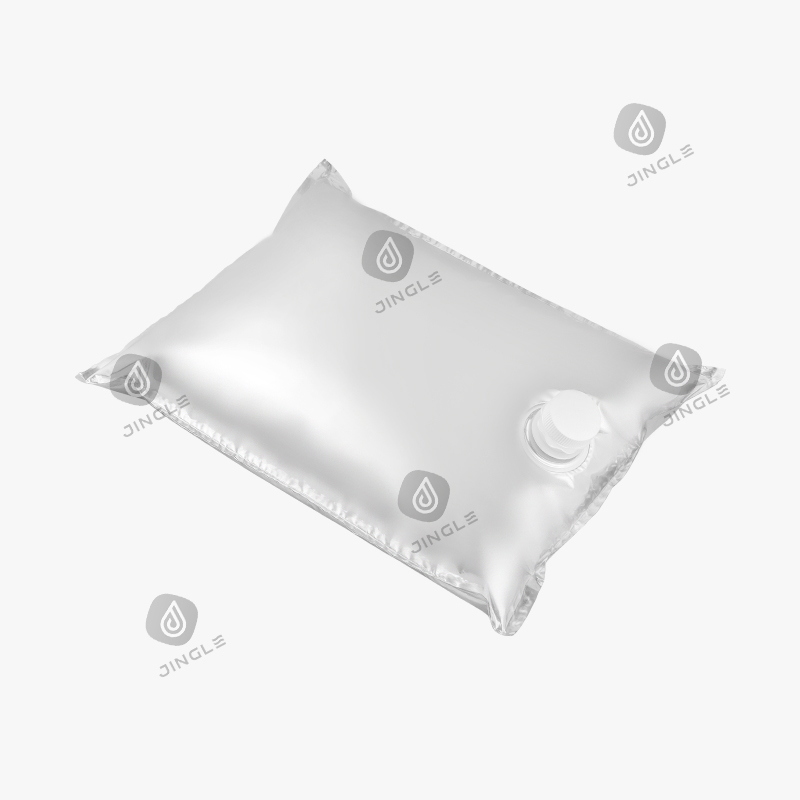
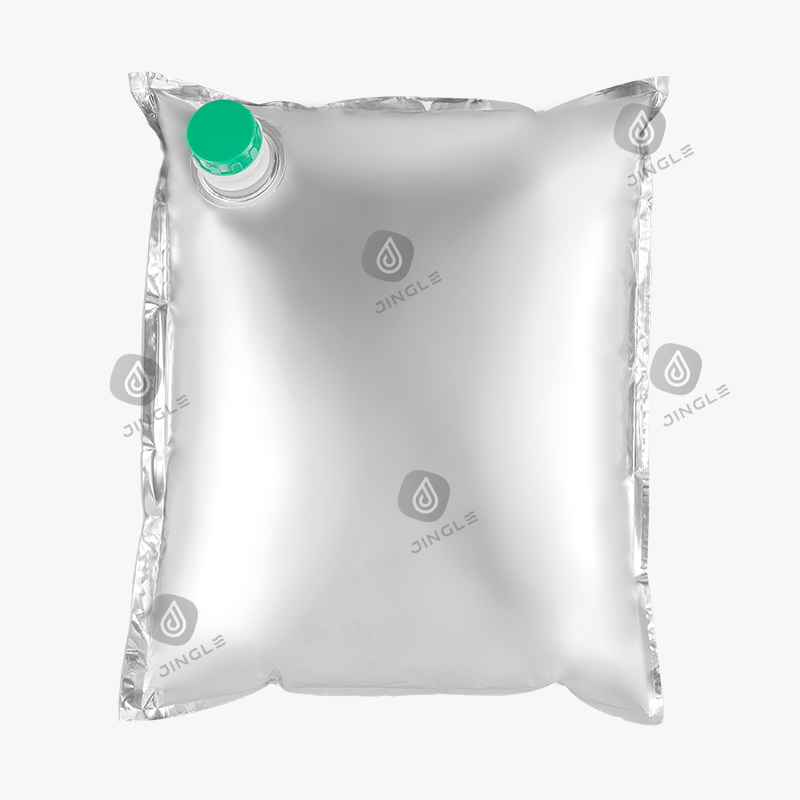
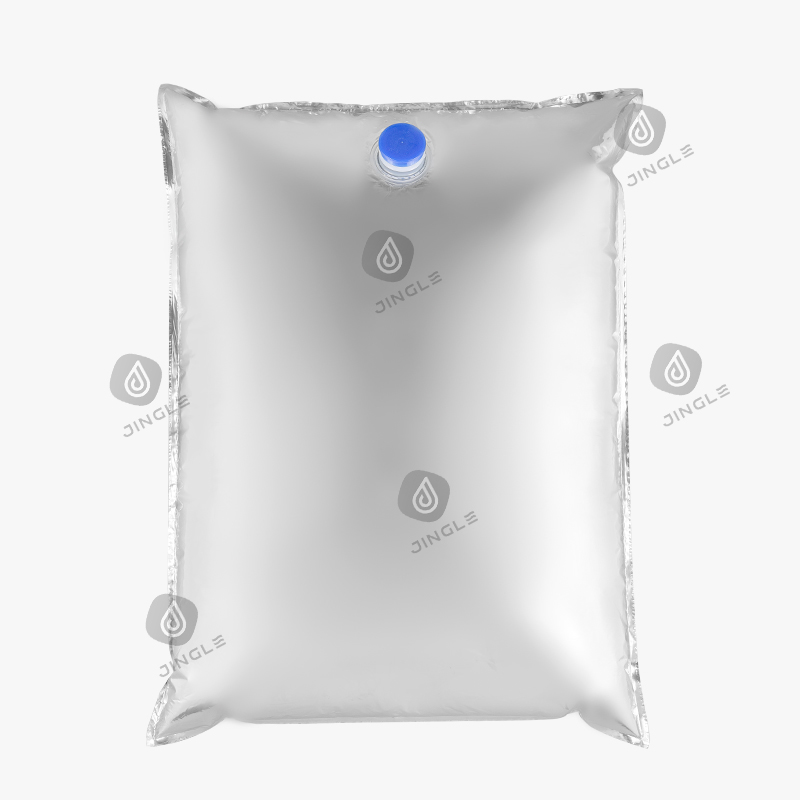
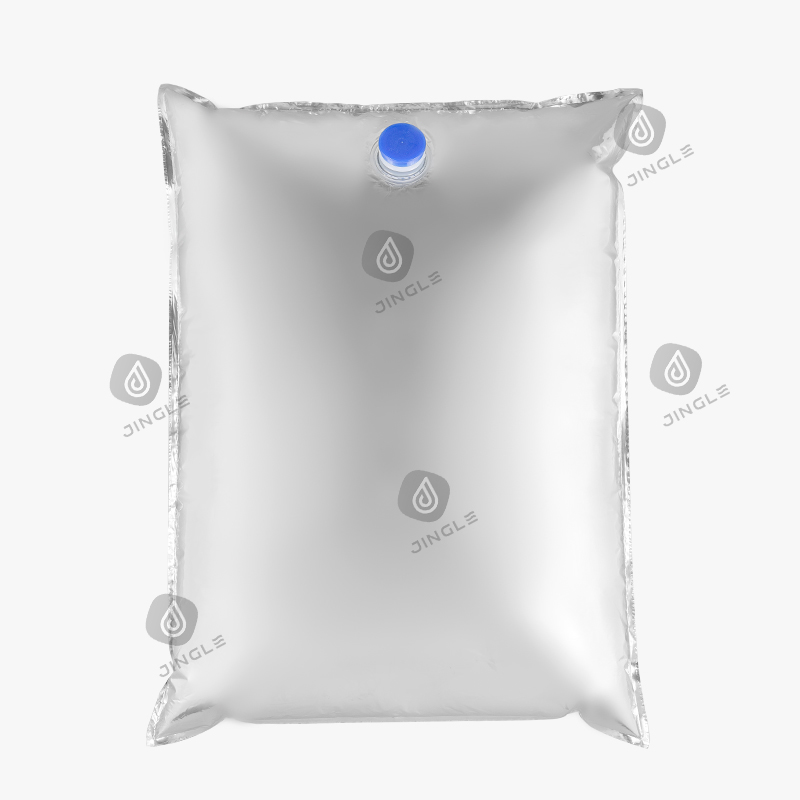
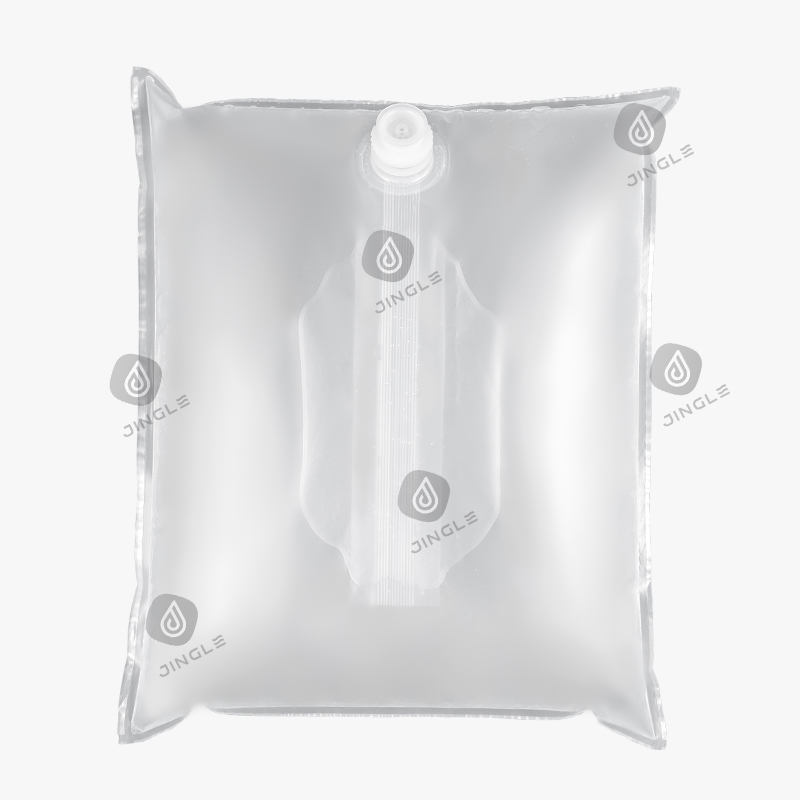
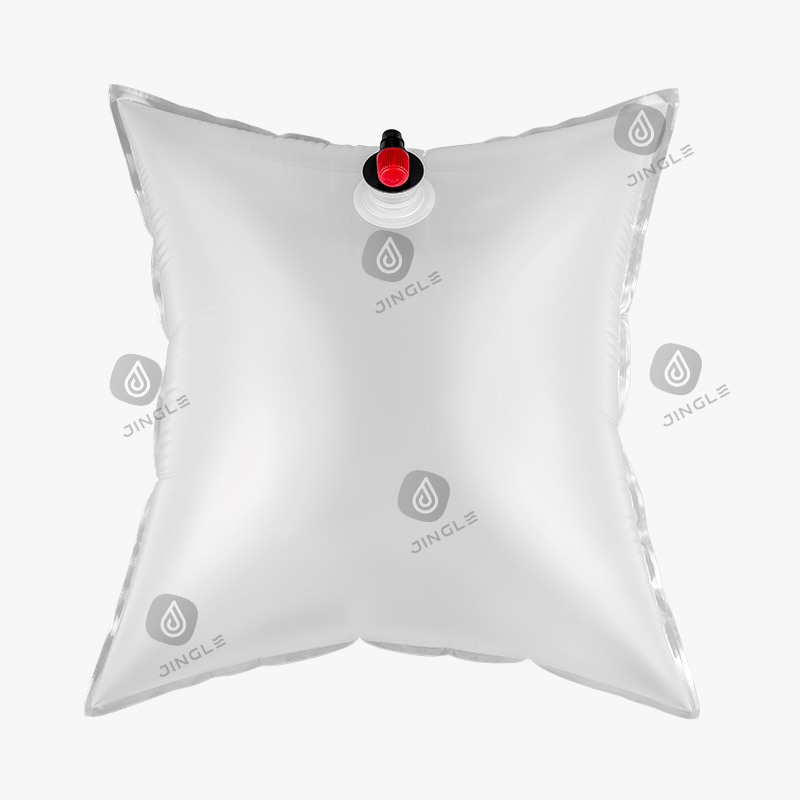
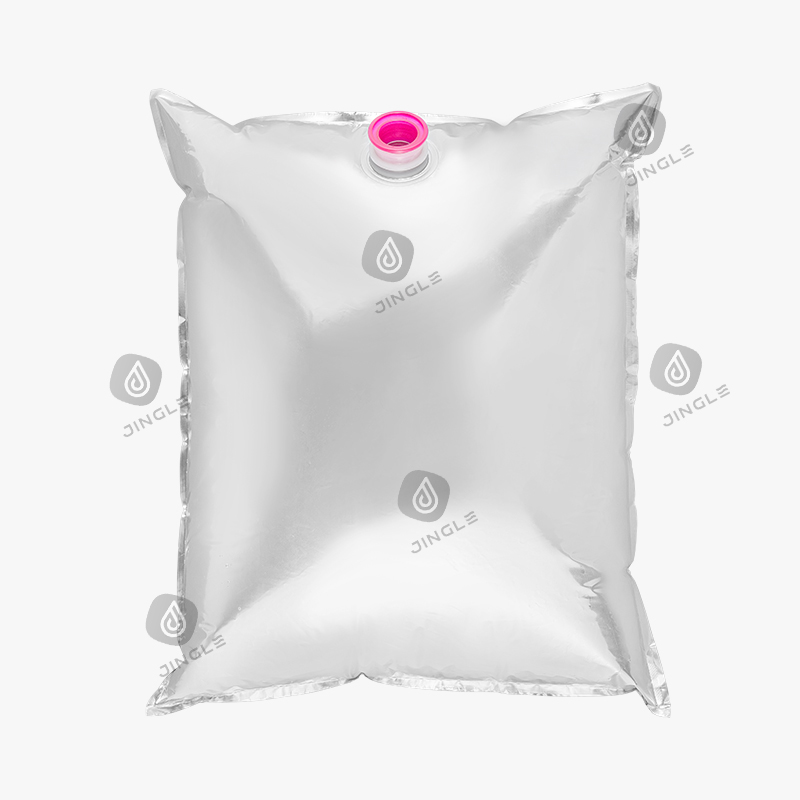
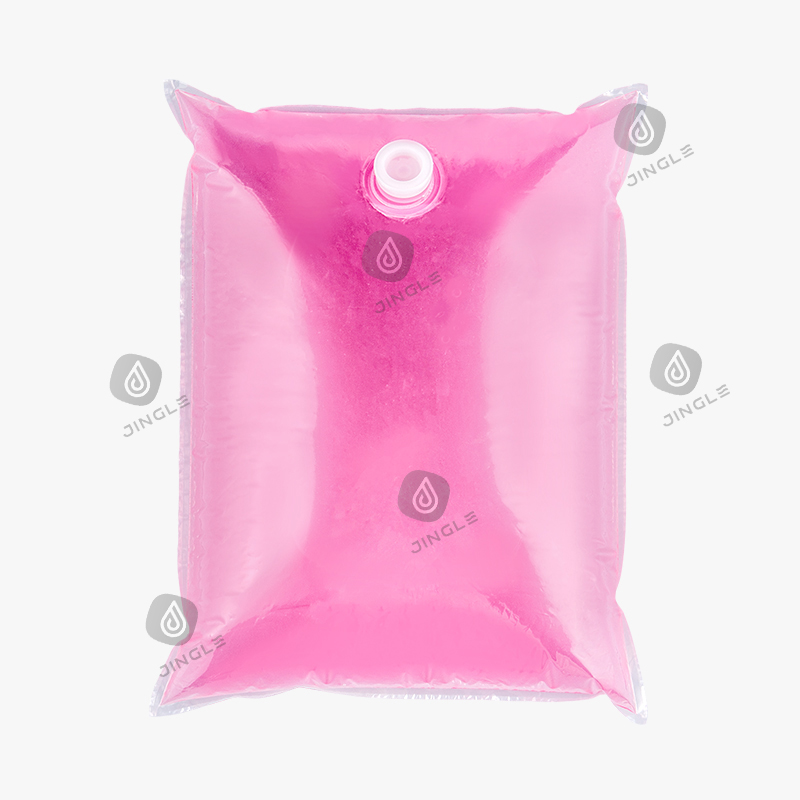
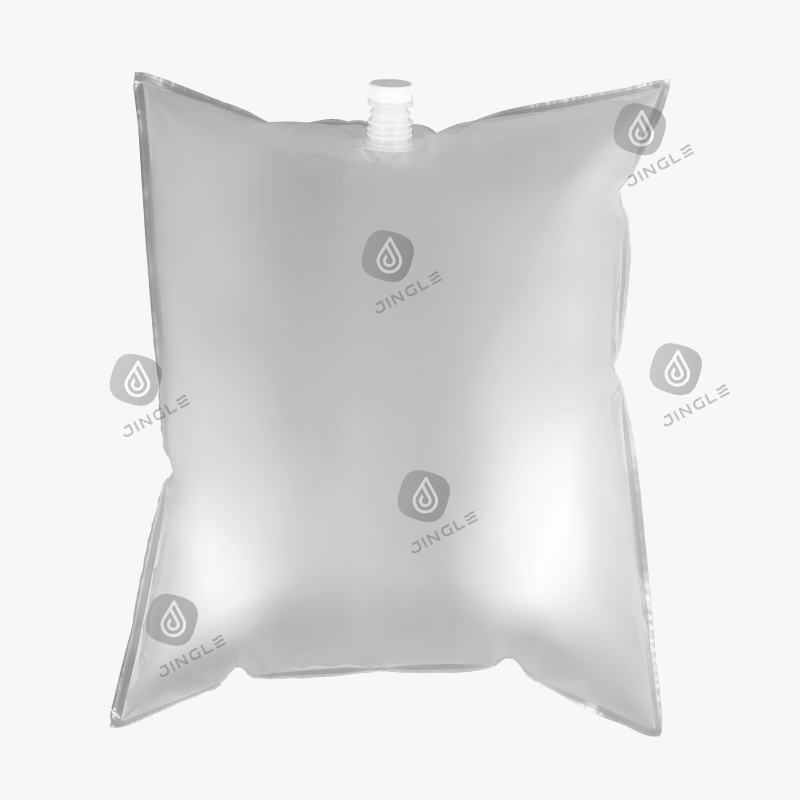
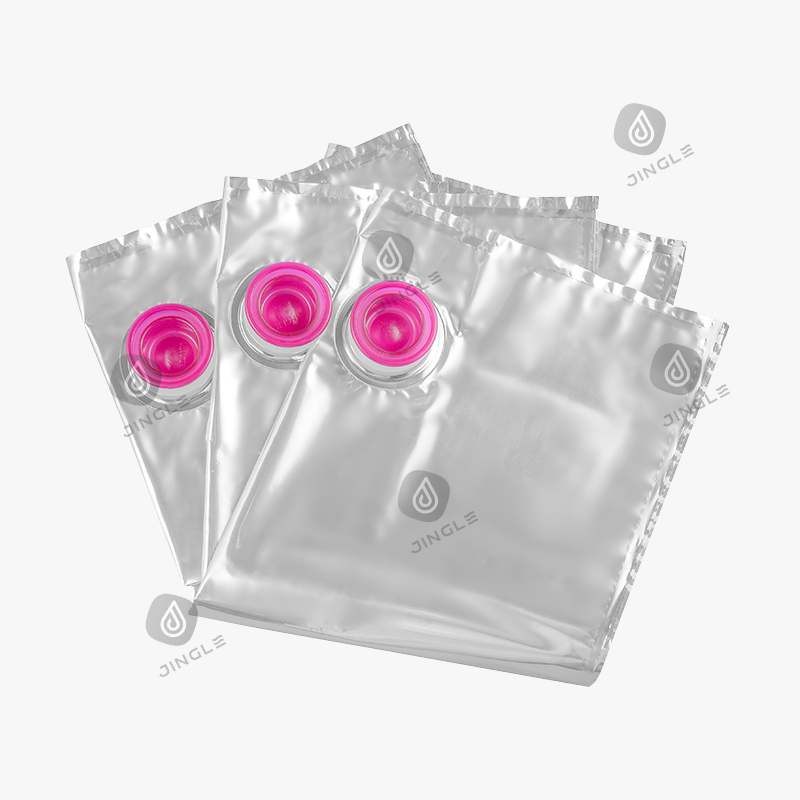
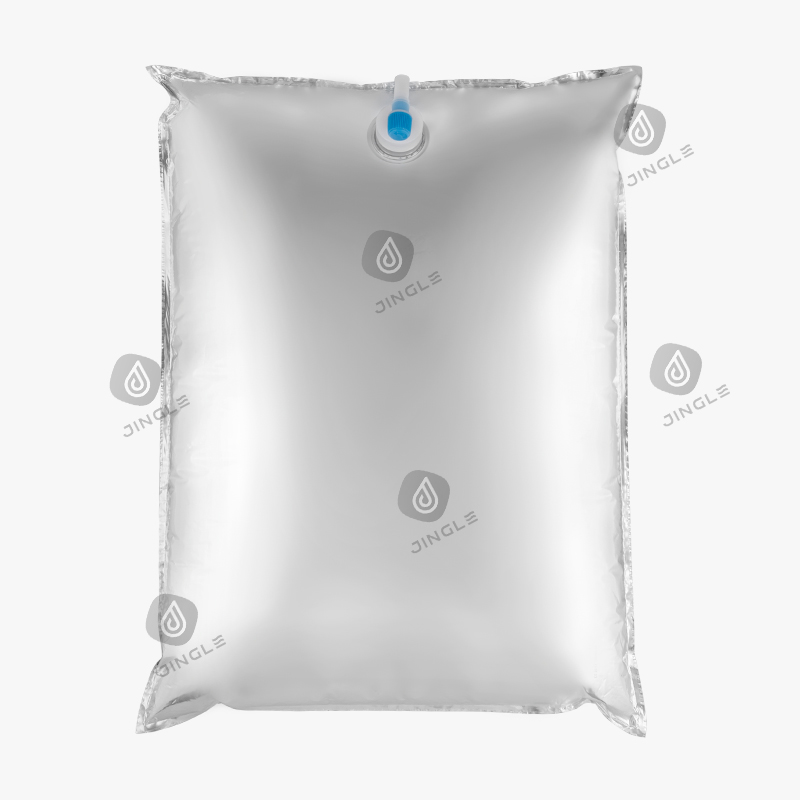
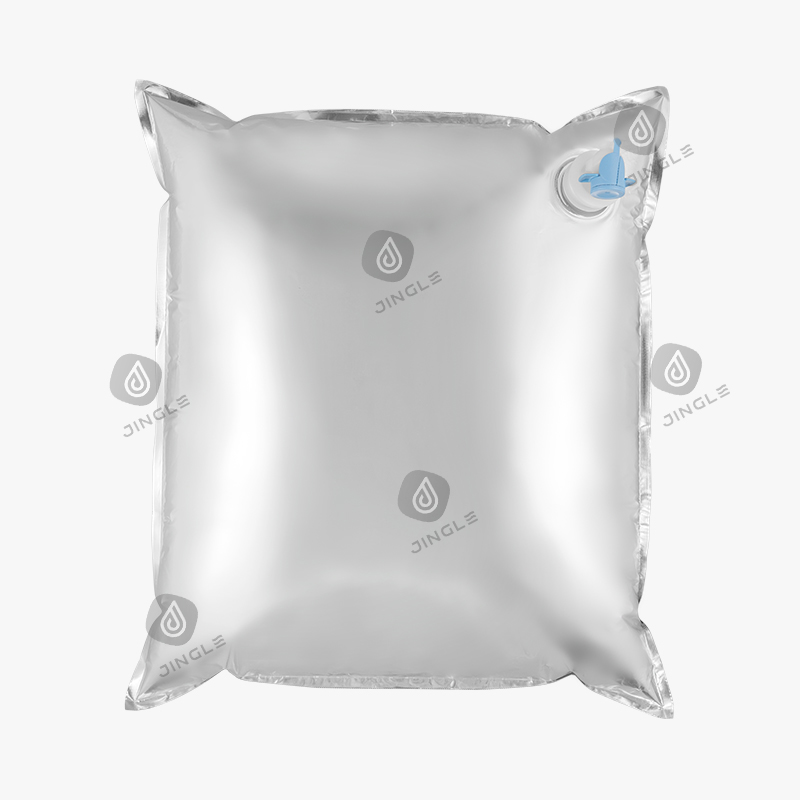
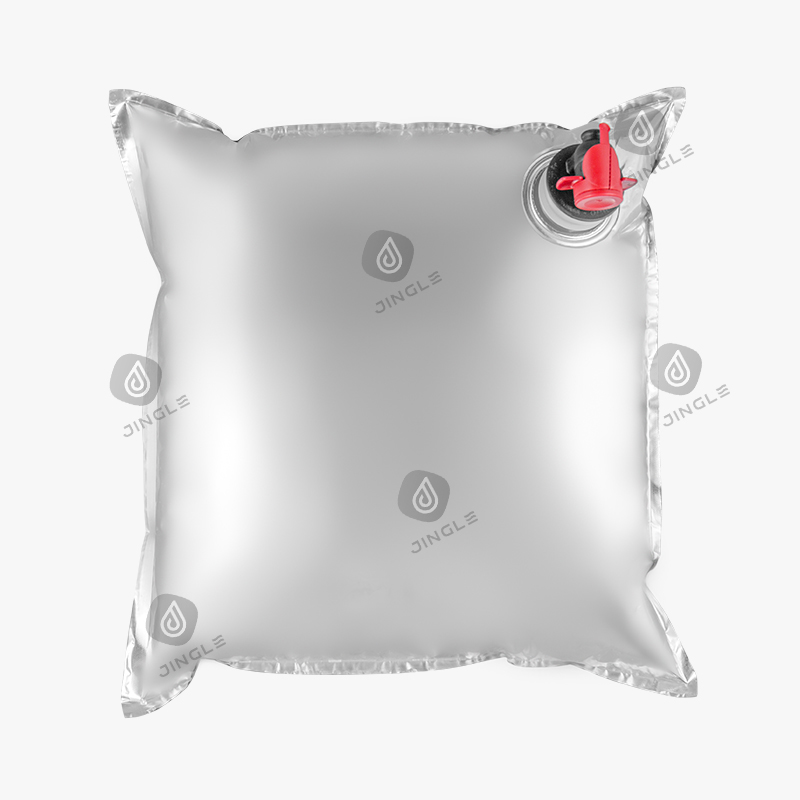
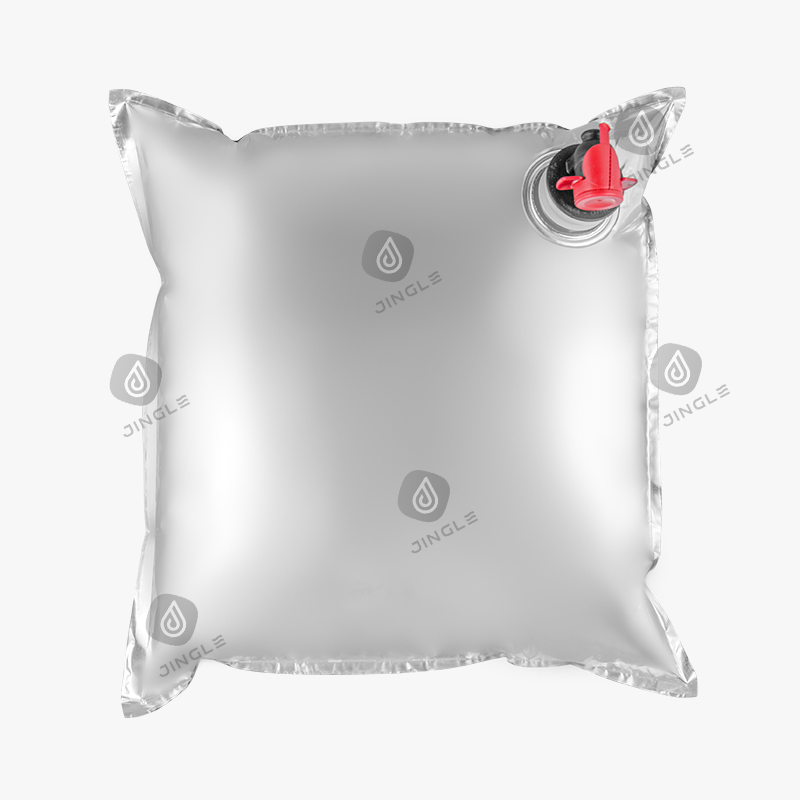
As a dedicated Dairy Bag-In-Box Packaging manufacturer, Suzhou Jingle Packaging Technology Co., Ltd. designs and produces bag-in-box (BIB) packaging specifically for liquid dairy products. Our range covers fresh milk, condensed milk, cream, yogurt drinks, and milk-based concentrates, with capacities from 3L to 20L and barrier film structures tailored to your product's oxygen sensitivity and distribution chain.
We operate an advanced BIB production line in our Suzhou factory, supported by a team with over 15 years of experience in liquid flexible packaging. From film co-extrusion to spout fitment and corrugated box assembly, we control the entire process to ensure food-grade safety and consistent quality. Our complete solution includes the packaging itself, compatible filling equipment, and after-sales support, so you can integrate a reliable packaging line without juggling multiple suppliers.
Why Dairy Products Need Specialized BIB Packaging
Dairy is highly vulnerable to oxygen, light, and microbial contamination, which cause fat oxidation, vitamin loss, and off-flavors. Standard polyethylene bags are insufficient for extended shelf life. Our dairy BIB bags use multi-layer co-extruded films with an EVOH oxygen barrier, achieving oxygen transmission rates below 2 cc/m²/24h—critical for UHT milk and other ambient-stable dairy products. For frozen dairy applications, we can specify films rated for sub-zero temperatures.
The bag-in-box format also offers practical advantages for commercial users:
- Extended post-opening shelf life: Airtight taps prevent oxygen ingress, maintaining product integrity for 3–6 weeks after opening.
- Reduced product residue: Collapsible bags allow near-complete evacuation, with residual volumes typically below 1% of total capacity.
- Lower logistics costs: Empty BIB components ship and store flat, reducing storage space by up to 60% compared to rigid containers.
- Material efficiency: Less packaging mass per liter reduces transport weight and material consumption.
Our Dairy BIB Product Range
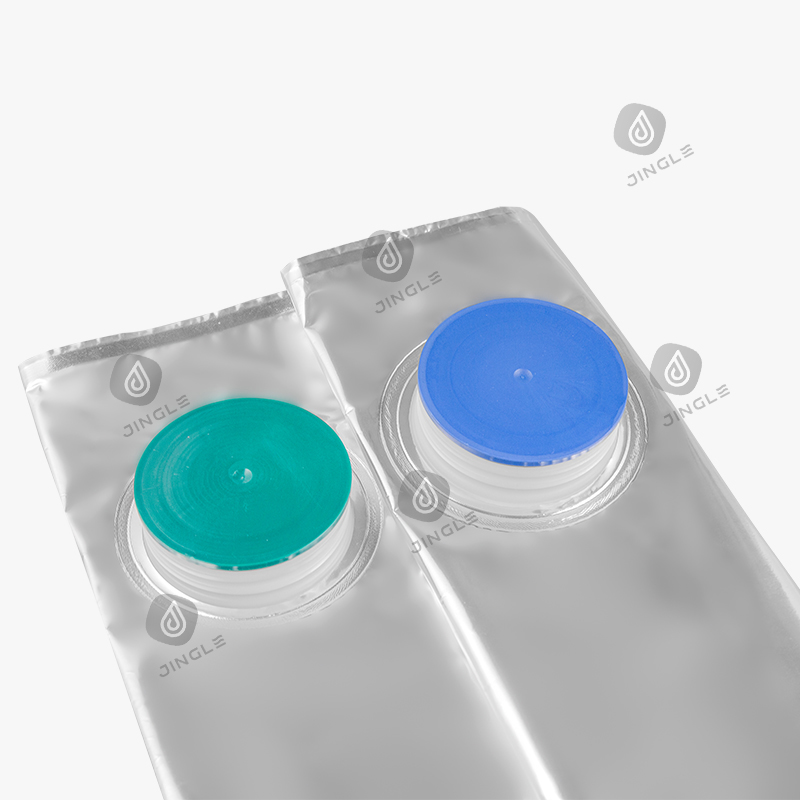
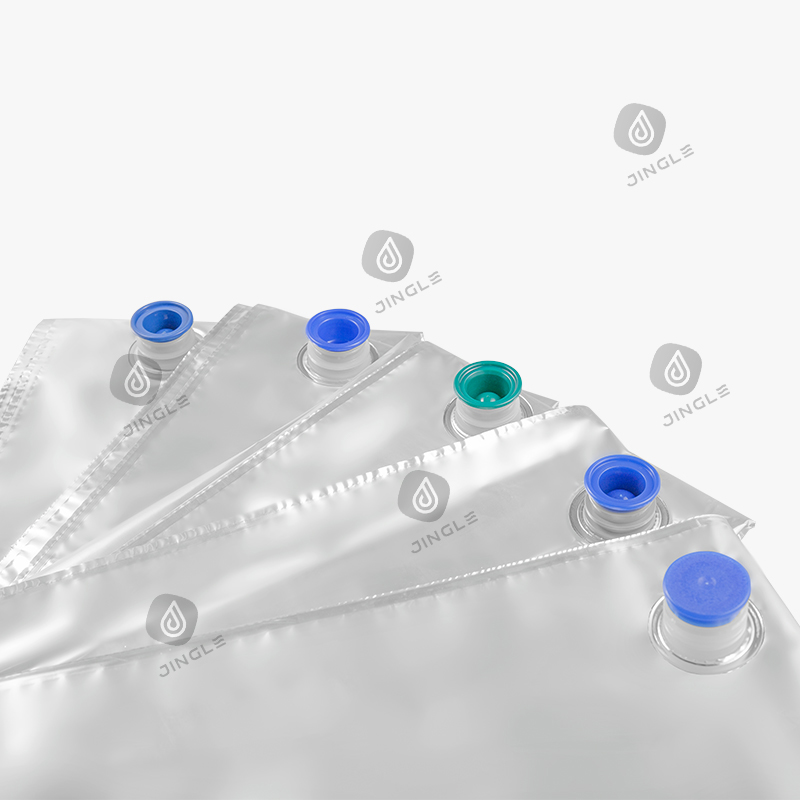
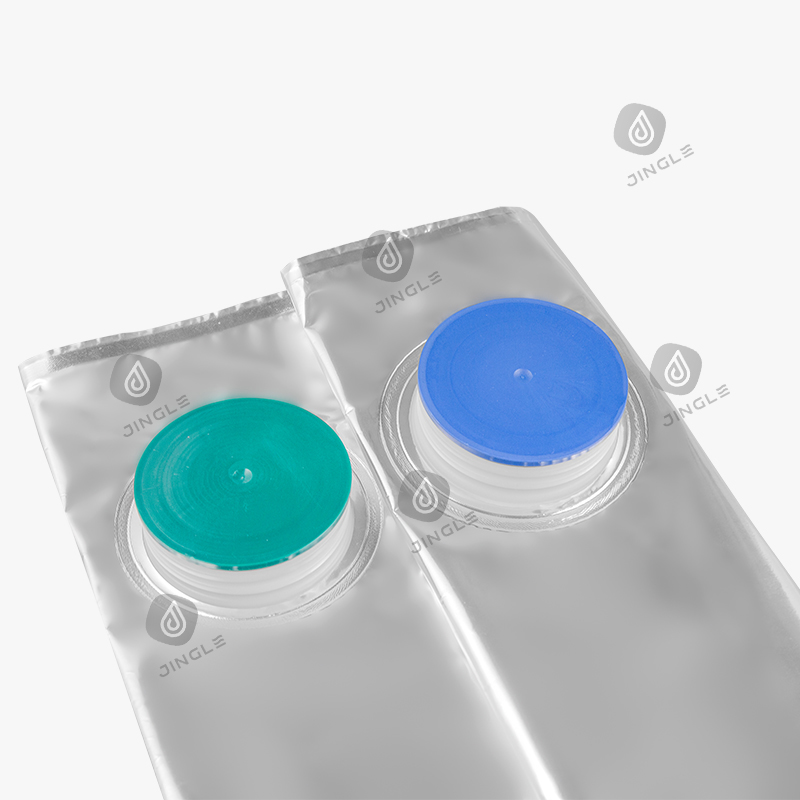
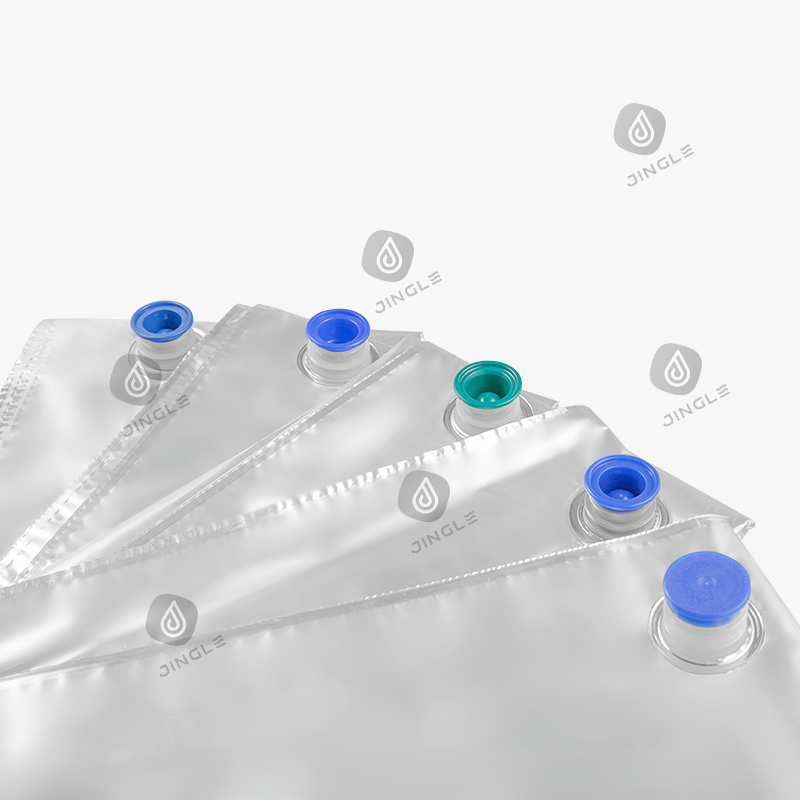
We supply complete BIB systems—bag, spout, tap, and corrugated box—configured to your filling line and end-use. The table below summarizes our standard options:
| Parameter |
Options / Range |
| Bag Film Structure |
Co-extruded PE with EVOH barrier, or Nylon/PE for high puncture resistance |
| Box Material |
Corrugated cardboard, single or double wall |
| Available Capacities |
3L, 5L, 10L, 12L, 15L, 20L |
| Tap Types |
Press tap, twist tap, push-pull tap (food-grade polymers) |
| Spout Fitment |
25mm or 32mm, compatible with standard filling machines |
| Filling Temperature |
4°C – 40°C (aseptic or non-aseptic filling) |
| Storage Temperature |
2°C – 8°C for fresh dairy; -25°C for frozen dairy |
Application Fit Across the Dairy Industry
Our dairy BIB packaging serves a wide range of operations, each with distinct requirements:
- Foodservice operations: High-volume milk dispensing for coffee shops, hotel breakfast buffets, and cafeterias. Our taps are designed for repeated use without dripping, and the bag collapses evenly to minimize waste.
- Dairy processing plants: Intermediate bulk storage and transport of liquid yogurt, cream, or milk concentrates. We can supply larger capacities and films that withstand the rigors of industrial handling.
- Commercial kitchens: Portion-controlled dispensing of dairy-based sauces, custard mixes, or batter preparations. The tap allows precise flow control, and the bag's barrier protects sensitive ingredients.
- Institutional catering: Schools, hospitals, and care facilities need consistent milk access without single-use cartons. Our BIB systems reduce packaging waste and simplify storage.
Technical Considerations for Your Filling Line
To ensure seamless integration, we confirm the following with your team before production:
- Filling compatibility: Our bags use standard spout fitments (25mm or 32mm) that work with most automatic filling machines. If you use a heat-seal interface, we can supply bags without spouts.
- Dispensing setup: For gravity dispensing, position the tap at least 10 cm above the dispensing area and elevate the box. For pump systems, confirm the outlet pressure rating (typically ≤0.5 bar) to avoid over-pressurizing the bag.
- Storage and handling: Store filled BIB units in a dry environment, stacked no more than 5 units high for 10L+ sizes. Do not freeze unless the film is rated for sub-zero temperatures.
- Ventilation: The corrugated box includes ventilation holes to allow the bag to collapse evenly. Ensure these are not blocked during storage or dispensing.
Quality Assurance and Compliance
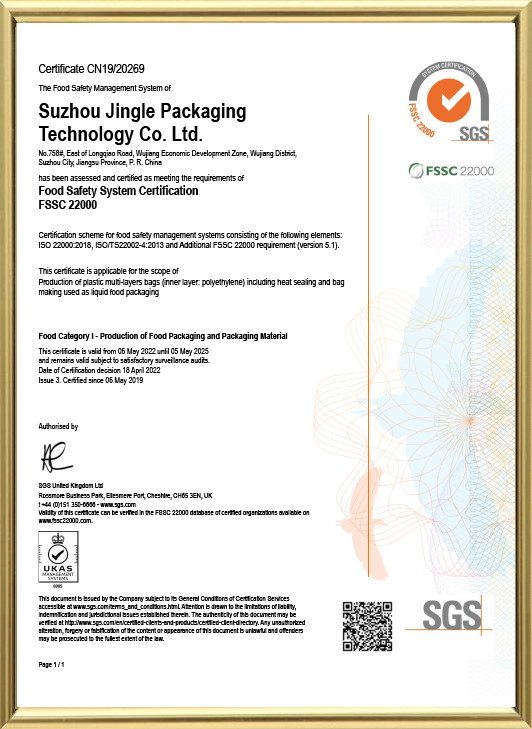
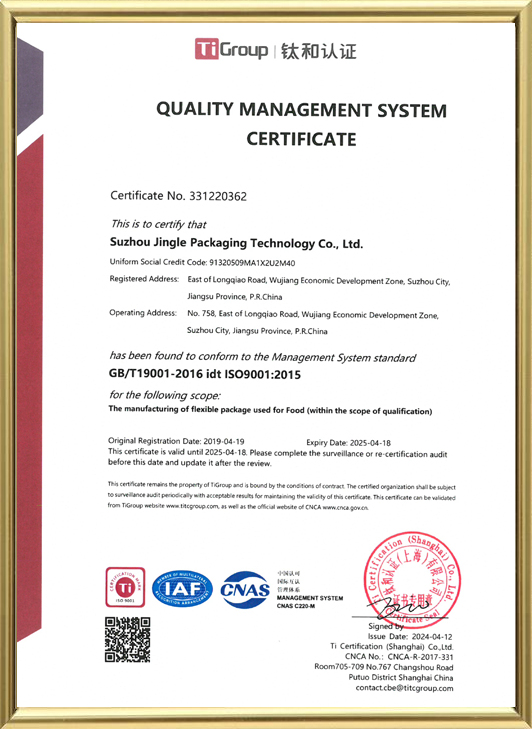
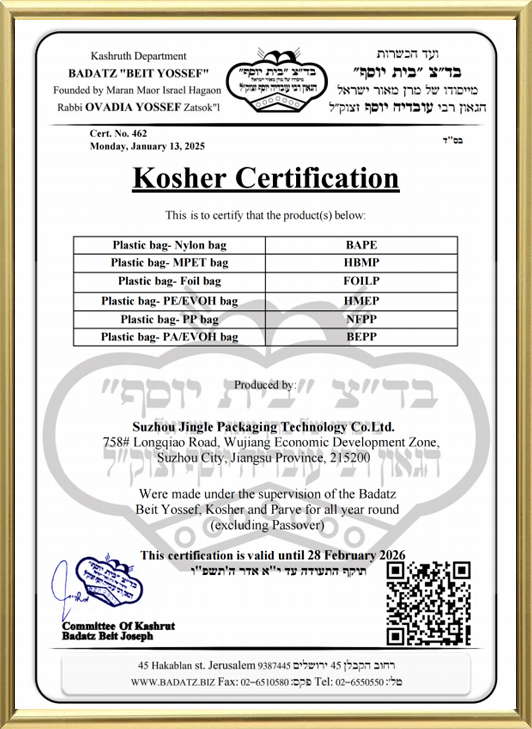
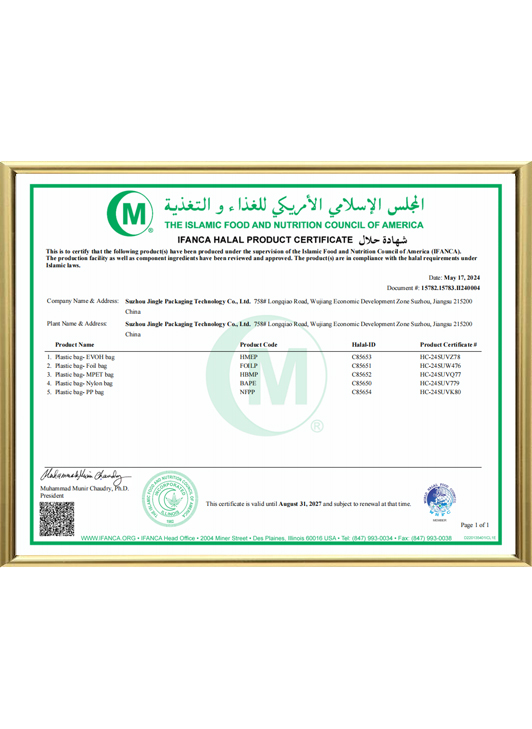
All our dairy BIB materials are food-grade and meet international safety standards. We hold SGS Quality Management System certification, and our products can be produced to comply with Kosher and Halal requirements when specified. Each production batch undergoes strict quality control, including seal integrity tests and barrier performance checks, to ensure consistent performance.
We also provide documentation for your own compliance needs, including material certificates and test reports. If you require specific certifications for your target market, we can discuss them during the quotation phase.
Information We Use to Configure Your Solution
To prepare an accurate proposal, we need the following details from your side:
- Product type: Fresh milk, UHT milk, cream, yogurt drink, concentrate, or other dairy liquid.
- Filling temperature and method: Aseptic or non-aseptic, and the temperature range of your product.
- Target shelf life: Required oxygen barrier level and storage conditions (ambient, chilled, or frozen).
- Capacity and box dimensions: Desired volume per unit and any space constraints in your distribution chain.
- Tap type and dispensing method: Press, twist, or push-pull; gravity or pump dispensing.
- Filling machine interface: Spout size (25mm or 32mm) or heat-seal requirement.
- Annual volume and order frequency: To optimize production planning and logistics.
With this information, we can recommend the optimal film structure, tap configuration, and box design, and provide a detailed quotation including packaging, filling equipment if needed, and delivery terms.
Frequently Asked Questions
What is the typical shelf life of dairy products in your BIB packaging?
For UHT milk with our EVOH barrier film, you can achieve ambient shelf life of 6–12 months, depending on filling conditions. For fresh dairy stored at 2–8°C, the package maintains quality for the expected chilled shelf life, and after opening, the tap preserves product integrity for 3–6 weeks.
Can you customize the bag size and tap type for our specific product?
Yes, we offer capacities from 3L to 20L and multiple tap types (press, twist, push-pull). We can also adjust the film structure to match your product's viscosity, fat content, and oxygen sensitivity. Send us your product specifications and we will recommend the right configuration.
Do you supply filling equipment that works with your bags?
Yes, we provide semi-automatic and fully automatic filling machines designed for BIB packaging. Our equipment is compatible with our spout fitments and can be integrated into your existing production line. We also offer installation support and after-sales service.
How do you ensure the bags meet food safety regulations?
All materials are food-grade and produced under SGS-certified quality management. We can provide material certificates and, if required, Kosher or Halal certification. Our production processes follow strict hygiene protocols to prevent contamination.
What is the minimum order quantity for custom dairy BIB packaging?
MOQ depends on the bag size and film structure. For standard sizes, we can accommodate smaller trial orders. For custom films or printing, a higher MOQ may apply. Contact us with your requirements and we will provide a specific MOQ.
How do you handle international shipping and delivery?
We are located in Suzhou, about 150 km from Shanghai Port, and we regularly export to Southeast Asia, Russia, Australia, and other regions. We can arrange sea freight, air freight, or express delivery based on your urgency. Our team will manage the export documentation and ensure your order arrives safely.
 English
 中文简体
 русский
 Español