Home / Products / BIB Packaging For Non-food Products
Suzhou Jingle Packaging Technology Co., Ltd.

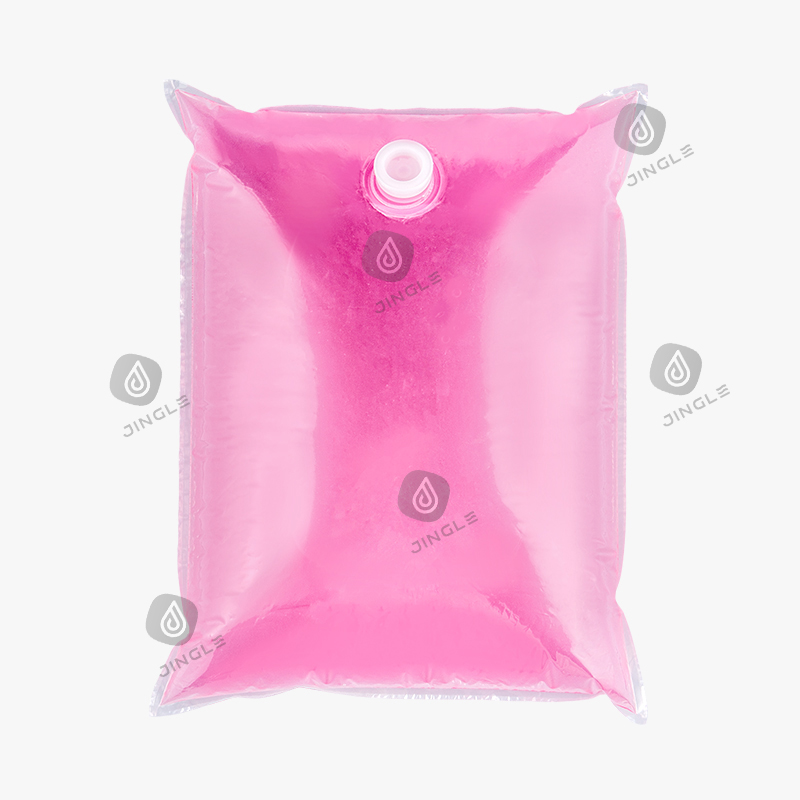
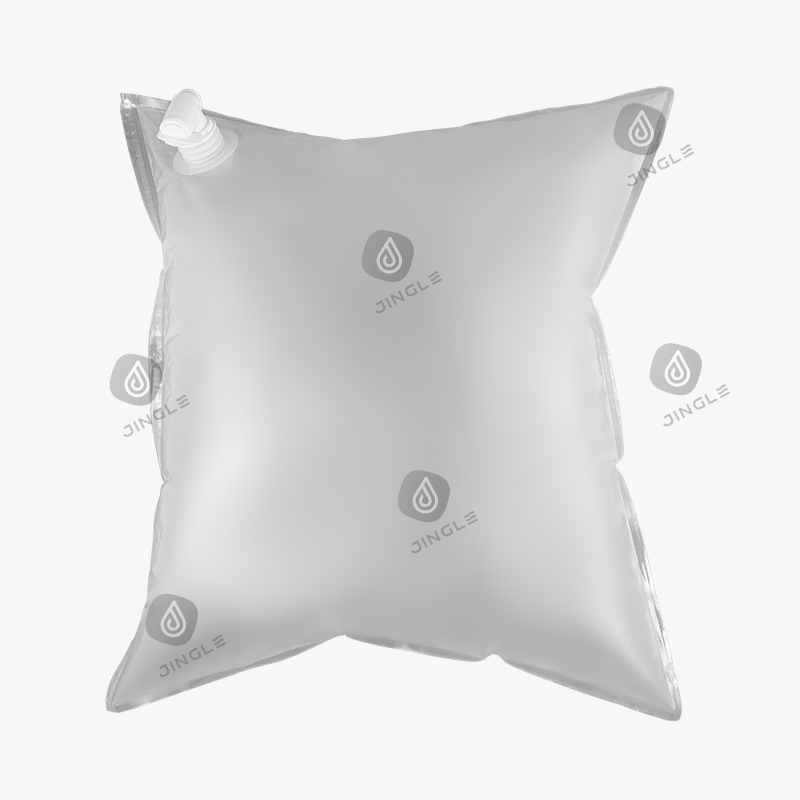
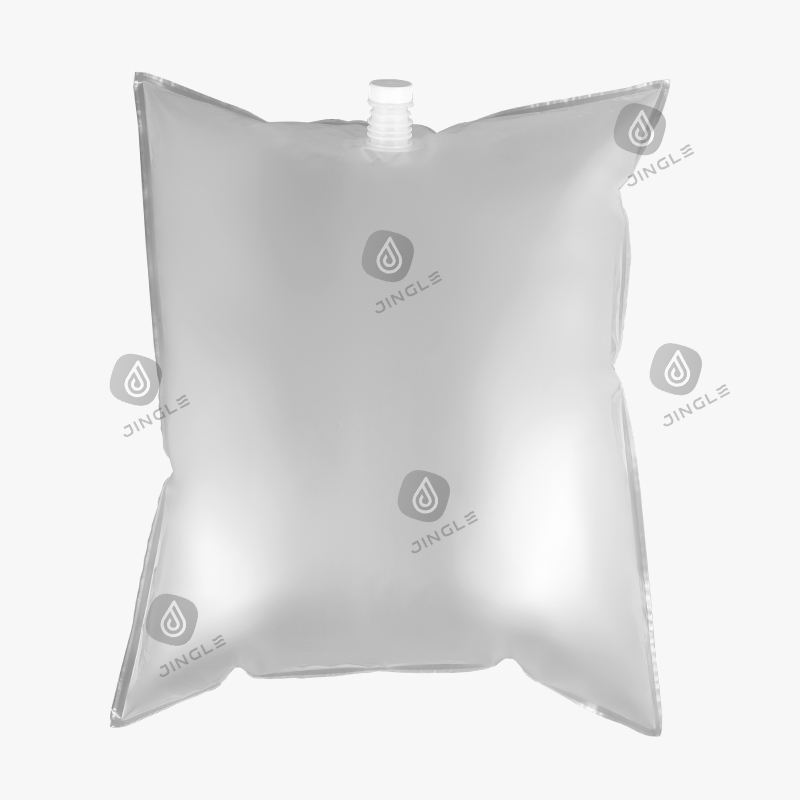
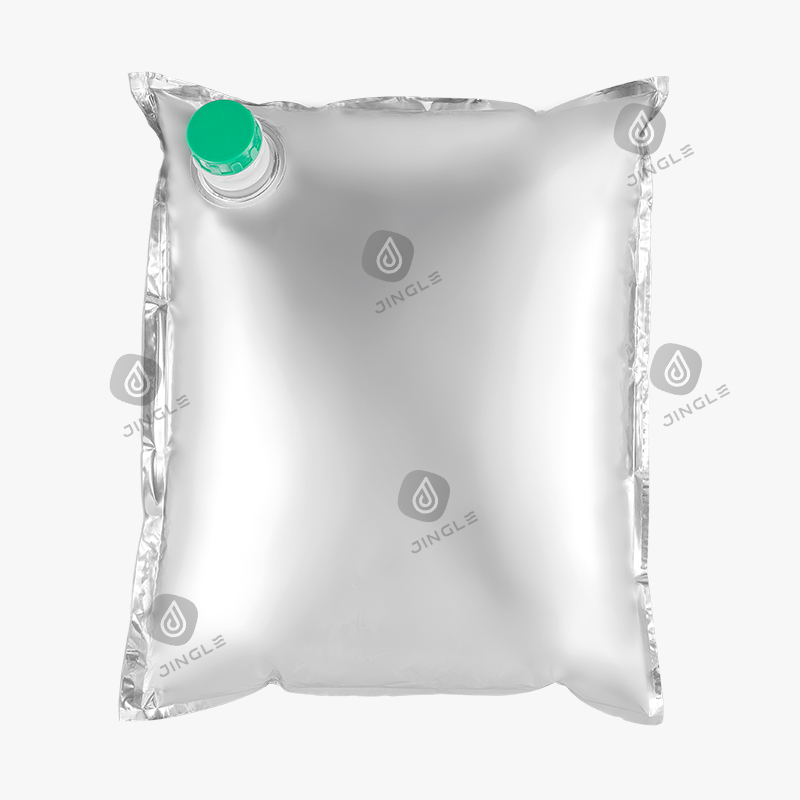
Custom BIB Packaging For Non-food Products

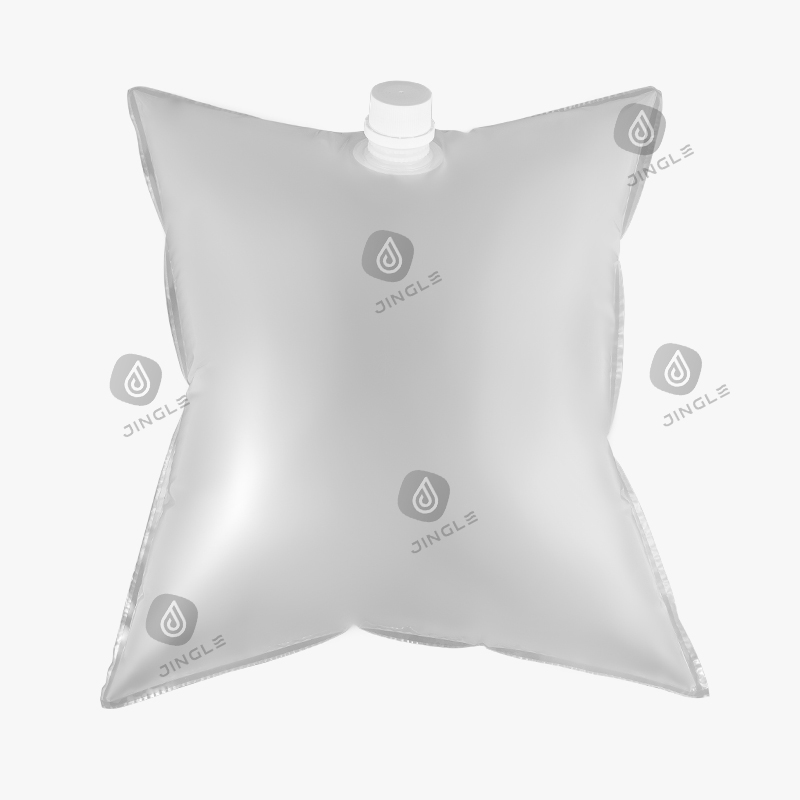
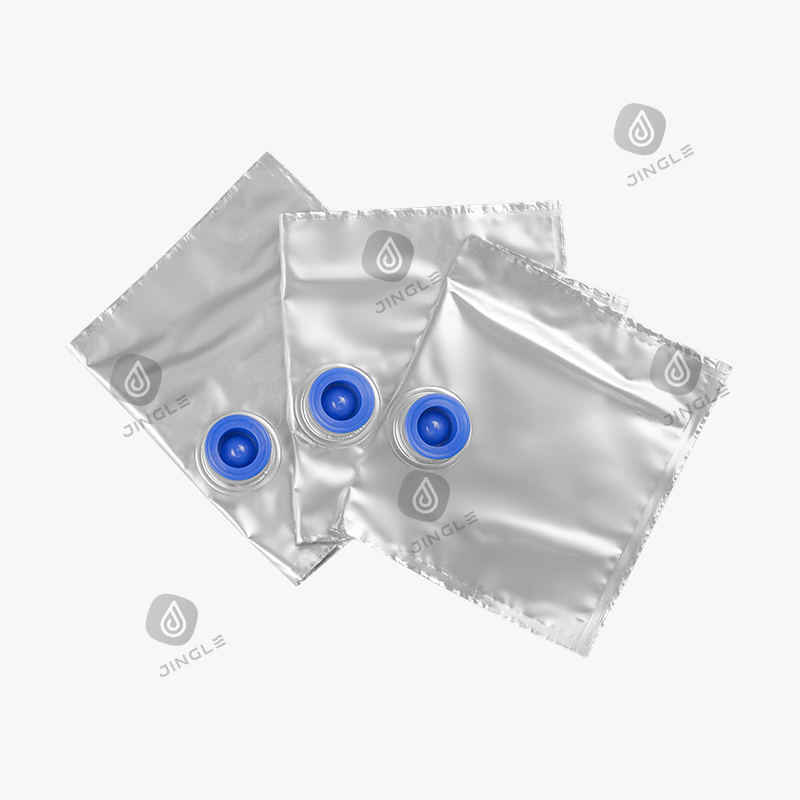
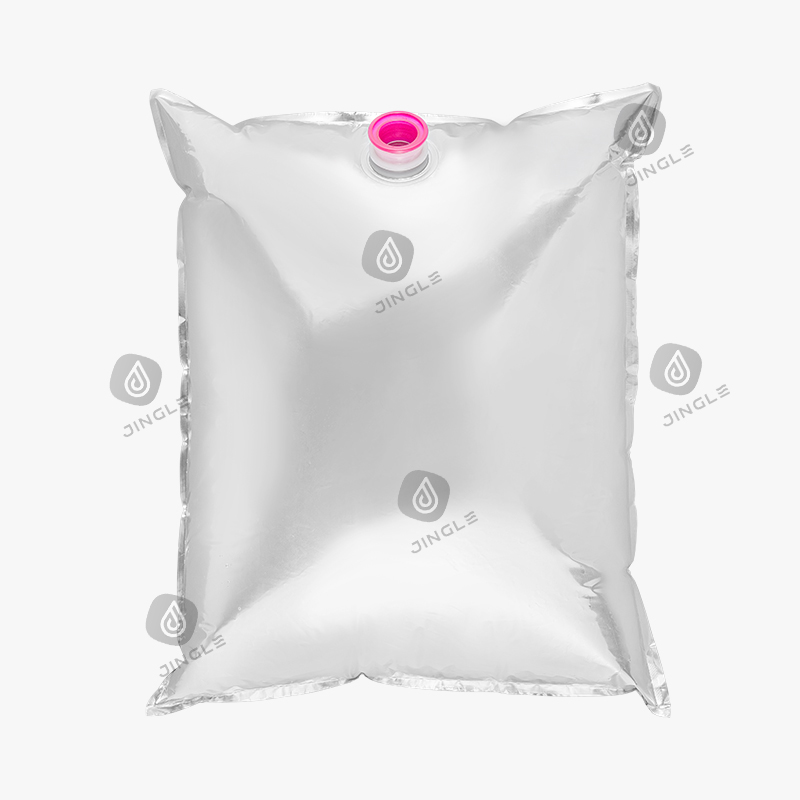
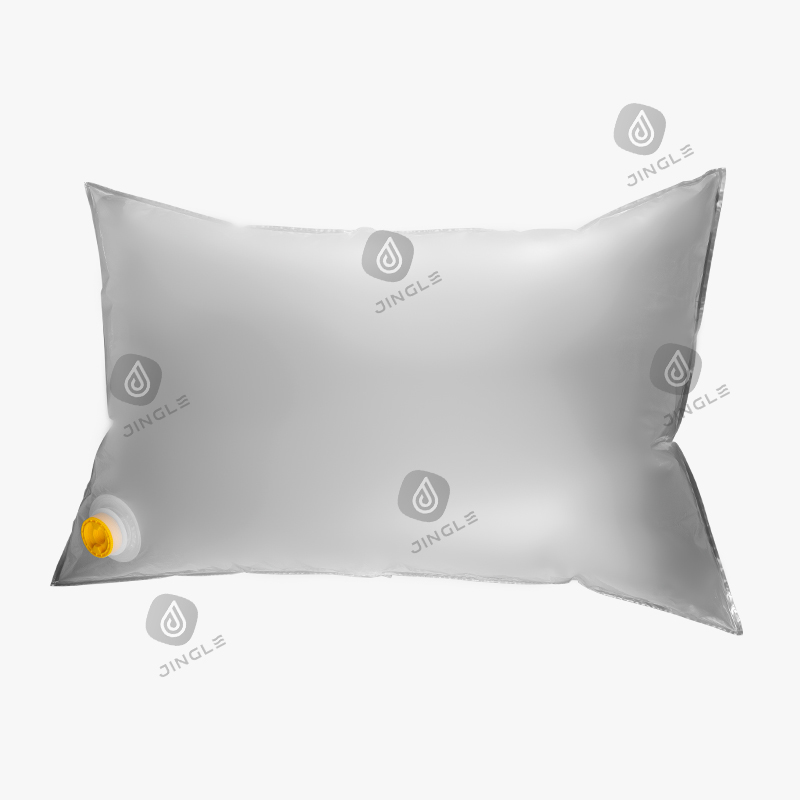
Non-sterile bags generally refer to products that are not sensitive to oxygen and humidity at room temperature, or products that are stored and transported by refrigeration/freezing, and packaging used for some agricultural chemicals, daily chemicals, motor oils, and other chemical products.

Pharmaceutical Intermediates
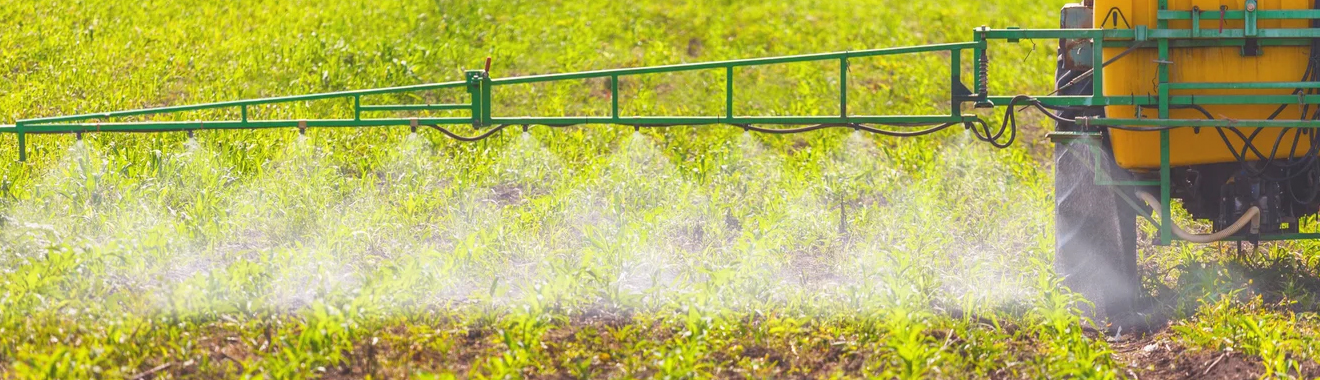
Agrochemical
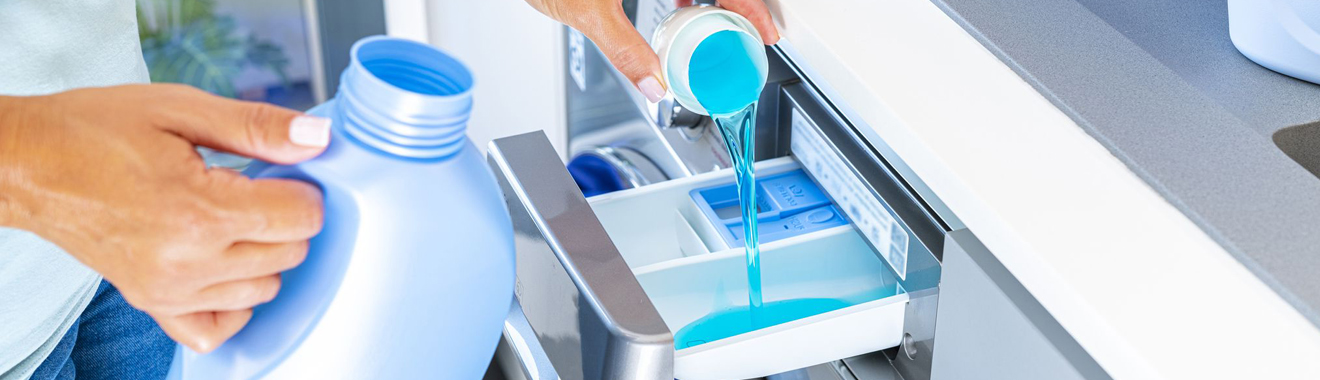
Daily Chemicals
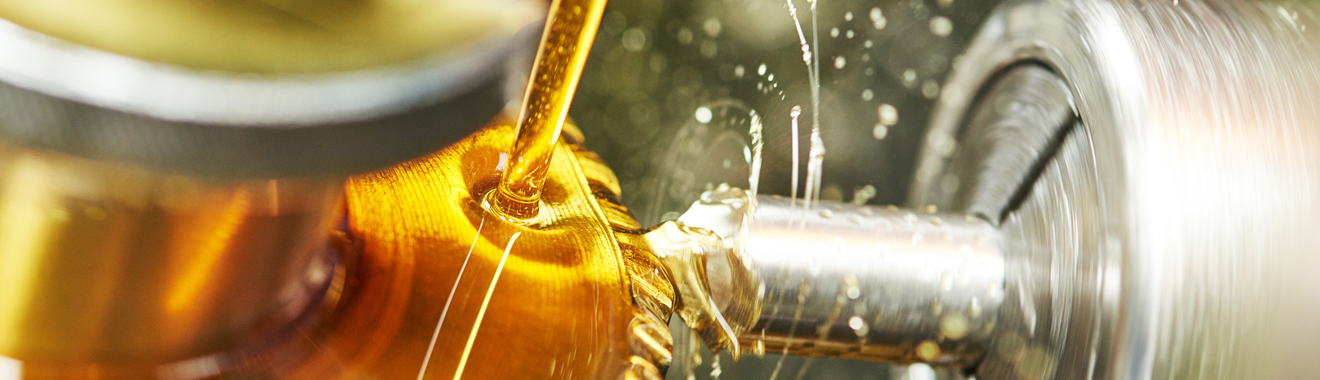
Car Supplies
Pharmaceutical Intermediates

Pharmaceutical Intermediates

Agrochemical

Agrochemical

Daily Chemicals

Daily Chemicals

Car Supplies

Car Supplies

Pharmaceutical Intermediates BIB Packaging

It can meet the product's demand for hygiene, select matching pharmaceutical films, and ensure good compatibility between packaging materials and contents, thereby ensuring the safety and effectiveness of the contents.

Agrochemical BIB Packaging

BIB packaging of pesticides makes it easier to dispose of the packaging after the drug is used up, reducing pollution to the environment.

Daily Chemicals BIB Packaging

BIB's large capacity + creative outer packaging carton, combined with different valves, can be used in offices, public areas, or homes. It is both practical and beautiful.

Car Supplies BIB Packaging

As the concept of environmental protection is deeply rooted in people's minds, BIB is gradually replacing traditional hard plastic packaging from the aspects of easy handling, environmental protection, and recyclability, and is emerging in the chemical industry.

Suzhou Jingle Packaging Technology Co., Ltd.
Industrial
Cleaning
Agriculture
Pharma
Non-Food Applications

BIB Packaging For Non-Food Products

Chemical-resistant flexible bulk containment for industrial lubricants, cleaning agents, agricultural chemicals, and pharmaceutical intermediates.

BIB packaging for non-food products extends the collapsible bag containment principle to industrial and institutional liquids requiring chemical compatibility verification. The inner bag film is selected based on the specific chemical properties of the product being contained.

Custom film formulations including fluorinated polyethylene, nylon laminates, and metallized barrier layers address solvent resistance, vapor transmission control, and pH stability requirements for non-food liquid products across multiple industrial sectors.

01
Chemical Compatibility Matrix Bag film materials are matched to product chemistry through compatibility testing. Options include fluorinated PE for solvent resistance, nylon laminates for hydrocarbon barrier, and acid-stable PE for low-pH cleaning concentrates.
02
Vapor & Odor Containment Metallized film layers block volatile organic compound (VOC) vapor transmission, reducing solvent loss and odor emissions during storage and dispensing.
03
Precise Dispensing Control Integrated taps and pump connectors enable metered dispensing of industrial liquids, reducing over-pour waste and chemical exposure risk for operators.
04
Hazardous Material Compliance UN-certified outer cartons and reinforced bag constructions meet dangerous goods packaging requirements for limited quantities of corrosive or flammable liquids.
Chemical Type
Film Recommendation
pH / Solvent Range
Typical Capacity
Water-Based Cleaners
Standard 3-ply PE laminate
pH 5–12
5L, 10L, 20L
Acid Cleaners
Acid-stable PE / PP inner layer
pH 1–5
5L, 10L
Solvent-Based Products
Fluorinated PE or nylon laminate
VOC 5–95%
3L, 5L, 10L
Agricultural Chemicals
EVOH barrier + UV-resistant outer
pH 3–10
5L, 10L, 20L
Pharma Intermediates
Clean-PE or fluorinated barrier film
pH 2–12
3L, 5L, 10L
01 Industrial Lubricants Bulk dispensing of cutting fluids, hydraulic oils, and machinery lubricants in manufacturing.
02 Cleaning Concentrates Janitorial and institutional cleaning chemical supply for dilution systems.
03 Agrochemical Dispensing Fertilizer concentrates and pesticide formulations for agricultural application.
04 Pharma Processing Intermediate storage of pharmaceutical liquids and excipients in production.
How to determine correct film for a solvent-based product? Submit product composition to the bag supplier for chemical compatibility testing. Key factors include solvent polarity, concentration, and expected storage temperature. Hydrocarbon solvents typically require fluorinated PE or nylon barrier layers to prevent film swelling and vapor loss.
Are BIB bags rated for corrosive chemical transport? Acid-stable PE films with pH tolerance down to 1.0 are available for corrosive cleaning concentrates. For UN-certified dangerous goods packaging, reinforced bag constructions and certified outer cartons meeting UN 4G or 4GV standards are required.
How to prevent vapor loss from volatile liquids? Metallized PET/PE laminate films reduce VOC vapor transmission to below 0.5 g/m²/day. For high-volatility solvents, specify bags with aluminum foil barrier layer and ensure the tap seal material is compatible with the solvent chemistry.
What disposal regulations apply to non-food BIB units? Bags containing hazardous chemical residues must be disposed per local hazardous waste regulations. Triple-rinse protocols may be required before recycling or disposal. Non-hazardous product bags can follow standard industrial plastic recycling streams after thorough rinsing.
Suzhou Jingle Packaging Technology Co. Ltd.

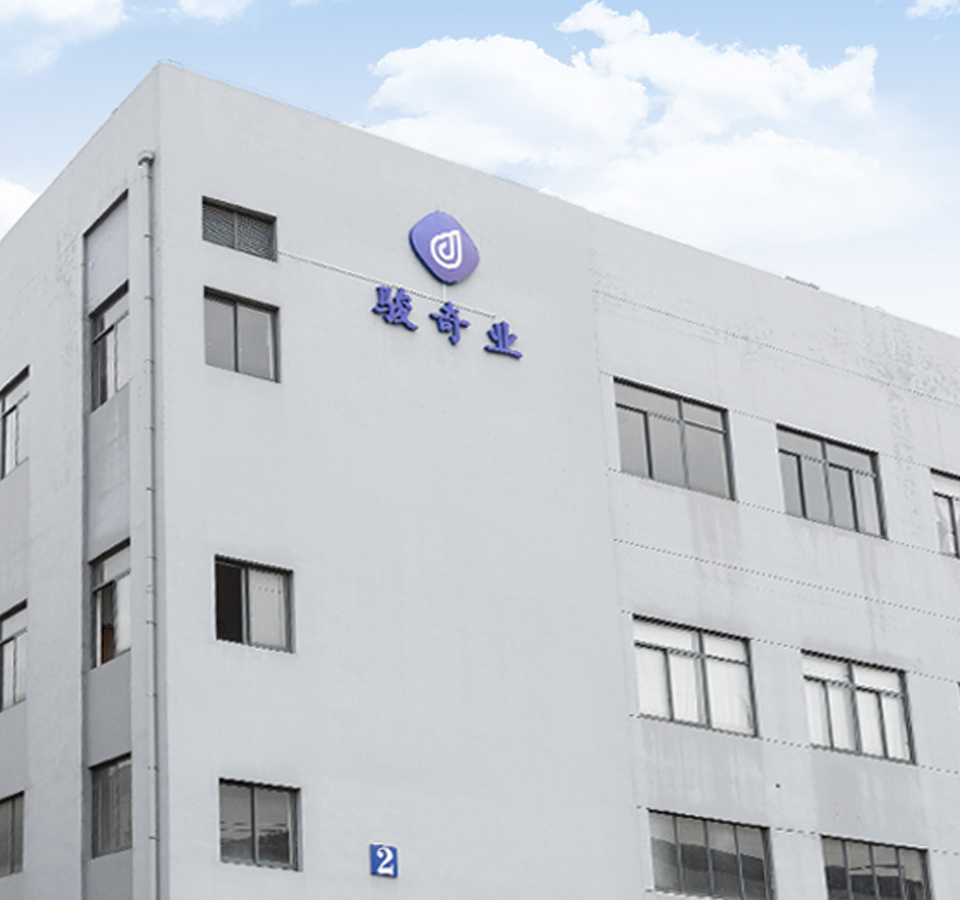
The company is located at No. 758, Longqiao Road, Wujiang Economic Development Zone, Suzhou, about 5 minutes' drive from the G15W Wujiang South Expressway Exit. The company is committed to providing high-quality products and all-round solutions to domestic and foreign customers, and actively exploring new markets with customers.
We are China BIB Packaging For Non-food Products Manufacturers and Custom BIB Packaging For Non-food Products Factory. The company has an advanced bag-in-box production line designed independently, which can produce products of various specifications according to customer requirements to meet customer supply needs.
It mainly develops and produces liquid flexible packaging products suitable for storing food, beverages, and non-food fields, as well as related supporting filling equipment, sells the products produced by the company, and provides corresponding after-sales services.

Suzhou Jingle Packaging Technology Co., Ltd.
Certificate Of Honor
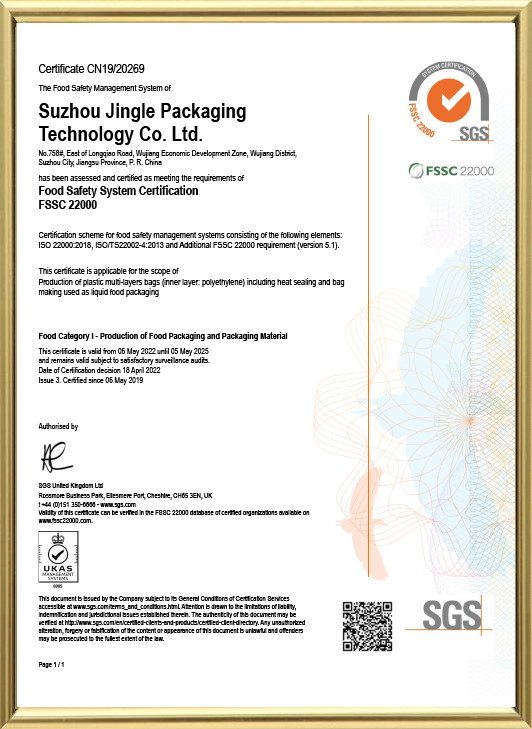
  • SGS
  • Quality Management System Certificate
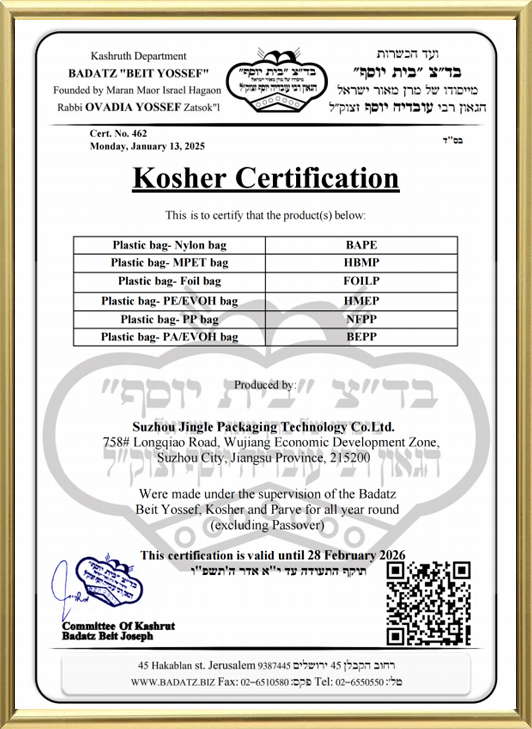
  • Kosher Certification
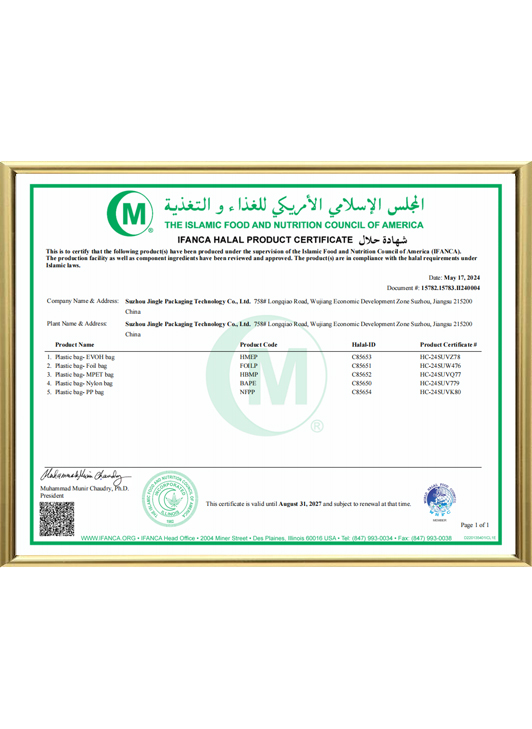
  • The Islamic Food And Nutrition Council Of America
News Center
Message Feedback
BIB Packaging For Non-food Products Industry knowledge

BIB Packaging For Non-food Products

Suzhou Jingle Packaging Technology Co., Ltd. is a China-based BIB Packaging For Non-food Products manufacturer and supplier. We design and produce flexible bag-in-box packaging for agrochemicals, pharmaceutical intermediates, daily chemicals, and car supplies, backed by our own production line and filling equipment support.

Our non-food BIB range is engineered for chemical resistance, vapor containment, and safe dispensing. We select inner bag films based on the product's chemistry, offering options from standard PE laminates to fluorinated PE and EVOH barriers. With over 15 years of industry experience, our team provides complete packaging solutions from film selection to carton design and filling integration.

Our Non-Food Product Range

We supply BIB packaging across four key non-food segments, each with specific film and connector requirements:

  • Agrochemical
    Pesticides, fertilizers, herbicides. UV-resistant films, UN-certified cartons, capacities 3L–20L.
  • Pharmaceutical Intermediates
    USP Class VI films, cleanroom manufacturing, ISO Class 7 filling, full traceability.
  • Daily Chemicals
    Detergents, cleaners, personal care. pH 2–14 tolerance, child-resistant taps, retail-ready cartons.
  • Car Supplies
    Motor oils, coolants, cleaning fluids. Chemical-resistant films, easy handling, recyclable.

Application Fit and Film Selection

Choosing the correct film is critical for non-food liquids. We match the inner bag to the chemical class, considering pH, solvent polarity, and storage temperature. Our compatibility testing follows ASTM D543 to verify film swelling and permeation resistance.

Chemical Type Film Recommendation pH / Solvent Range Typical Capacity
Water-Based Cleaners Standard 3-ply PE laminate pH 5–12 5L, 10L, 20L
Acid Cleaners Acid-stable PE / PP inner layer pH 1–5 5L, 10L
Solvent-Based Products Fluorinated PE or nylon laminate VOC 5–95% 3L, 5L, 10L
Agricultural Chemicals EVOH barrier + UV-resistant outer pH 3–10 5L, 10L, 20L
Pharma Intermediates Clean-PE or fluorinated barrier film pH 2–12 3L, 5L, 10L

Critical Specifications and Options

We configure each BIB unit to your product's requirements. Key parameters include:

  • Capacity: From 1L to 20L standard, with custom sizes for process integration.
  • Barrier layers: Metallized PET/PE, aluminum foil, or EVOH for VOC and oxygen control.
  • Connectors: 25mm or 32mm spouts, dry-lock quick-disconnects, child-resistant taps, or aseptic fittings.
  • Outer carton: Single or double-wall corrugated, with UN 4G/4GV certification for dangerous goods.

For volatile liquids, metallized films reduce vapor transmission to below 0.5 g/m²/day. For corrosive chemicals, acid-stable PE tolerates pH down to 1.0. Our engineering team helps you select the right combination.

Quality Assurance and Compliance

Our factory in Wujiang Economic Development Zone operates an advanced bag-in-box production line with strict quality control. We hold SGS quality management certification and offer documentation for regulatory submissions.

For non-food applications, we provide:

  • Chemical compatibility test reports per ASTM D543.
  • UN 4G/4GV certification for hazardous liquid transport.
  • USP Class VI and ISO Class 7 cleanroom options for pharmaceutical intermediates.
  • Batch traceability and certificates of conformance.

Integration with Filling Equipment

We supply not only packaging but also semi-automatic and fully automatic filling machines. Our team assists with line integration, ensuring your BIB bags fill accurately and efficiently. We provide after-sales support and spare parts for all equipment.

Information We Use to Configure Your Solution

To prepare a precise proposal, we need the following details from you:

  • Product name and chemical composition (including pH, solvent content, viscosity).
  • Required capacity per bag and target filling volume.
  • Storage and transport conditions (temperature, humidity, stacking).
  • Dispensing method (tap, pump, or connector type).
  • Regulatory requirements (UN certification, USP Class VI, etc.).
  • Production volume and line speed expectations.

With this information, we can recommend the optimal film structure, carton design, and filling solution.

FAQs

How do I determine the correct film for a solvent-based product?

Submit your product composition for chemical compatibility testing. Key factors include solvent polarity, concentration, and storage temperature. Hydrocarbon solvents typically require fluorinated PE or nylon barrier layers to prevent film swelling and vapor loss.

Are BIB bags rated for corrosive chemical transport?

Yes, acid-stable PE films with pH tolerance down to 1.0 are available for corrosive cleaning concentrates. For UN-certified dangerous goods, we use reinforced bag constructions and certified outer cartons meeting UN 4G or 4GV standards.

How do you prevent vapor loss from volatile liquids?

We use metallized PET/PE laminate films that reduce VOC vapor transmission to below 0.5 g/m²/day. For high-volatility solvents, we recommend an aluminum foil barrier layer and ensure the tap seal material is compatible with the solvent chemistry.

What disposal regulations apply to non-food BIB units?

Bags containing hazardous chemical residues must be disposed of per local hazardous waste regulations. Triple-rinse protocols may be required before recycling. Non-hazardous product bags can follow standard industrial plastic recycling streams after thorough rinsing.

Can you provide custom sizes and printing?

Yes, we specialize in custom solutions. We can adjust bag dimensions, capacity, film layers, and print full-color graphics on the outer carton. Provide your drawings or samples, and we will develop the packaging accordingly.

Related Products and Categories

Our portfolio also includes Lub Oil, BIB Packaging For Food & Beverage, Dairy for applications with different operating ranges, interfaces or integration requirements.